
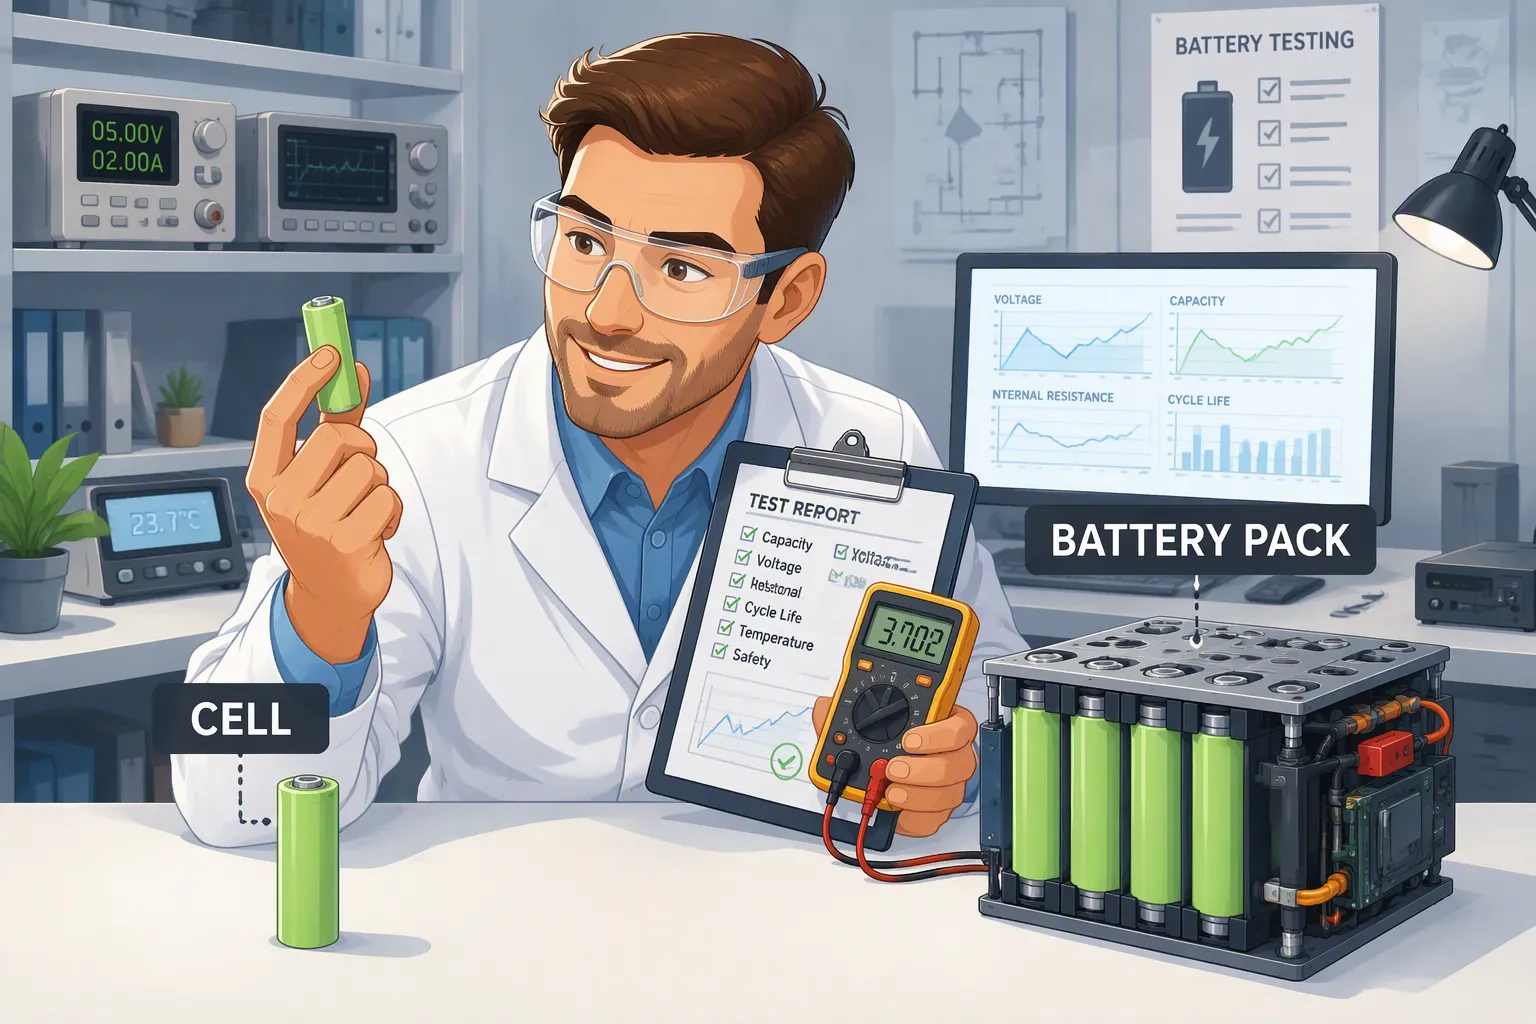
A cell test report describes the identified cell samples under stated conditions. A battery pack report addresses the assembly within its defined test scope. Neither should be assumed to establish every aspect of the finished device’s safety or performance.
For OEM buyers, the task is to connect the evidence to the product being purchased: exact cell model, pack configuration, protection electronics, drawing revision and intended application. A familiar laboratory logo or a “PASS” on a cover page is not enough.
Quick Answer: Verify who issued the document, what samples and revisions it covers, which standard and edition were used, the tests performed and any limitations. Cross-check cell identification against the pack bill of materials and the shipped assembly. Distinguish design qualification from production inspection, and obtain a documented change assessment when the supplied design differs from the tested configuration.
Key Takeaways
Cell evidence supports component selection but does not automatically qualify the assembled pack.
A certificate, test report, transport test summary and production inspection record serve different purposes.
Choose standards by application and market rather than applying automotive requirements to every battery.
Destructive safety tests normally use designated samples, not every saleable unit.
Design changes require review; they do not automatically invalidate every report or certificate.
Part 1: Battery Cell vs Battery Pack Test Reports Defined
1.1 What Each Evidence Level Can Establish
Cell reports may include capacity, resistance, cycle performance or safety tests, depending on their purpose. Pack reports may examine charging, protective functions, interconnects, mechanical behavior or environmental performance. Read the actual scope: the document title does not prove that all these subjects were evaluated.
Device integration adds another level. The host’s charger, load, mounting, heat sources, alarms and firmware can affect battery behavior. Pack qualification does not replace verification of runtime, charging and relevant safety functions in the intended device.
Evidence | Main question | Important limitation |
|---|---|---|
Cell test report | How did the identified cells perform in specified tests? | Does not automatically address pack construction |
Pack test report | How did the identified assembly perform? | May not cover the host device or every production variant |
Device validation | Does the integrated product meet its requirements? | Applies to the evaluated system and conditions |
Production inspection record | Did the inspected units meet release criteria? | Does not replace design or lifetime qualification |
1.2 Distinguish Reports from Certificates and Summaries
A test report records methods, samples and results. A certification document identifies approval under a defined scheme and scope. A supplier declaration is another form of evidence and should not be described as independent certification. A UN 38.3 test summary is a standardized transport document, not the complete test report.
Laboratory accreditation and product certification are also different. Accreditation concerns competence for activities within a stated scope; it does not certify every product tested by the laboratory. Quality-management certification concerns the organization’s system and does not prove a specific battery passed a product test.
Part 2: Why OEM Buyers Need Linked Evidence
2.1 What Cell-Only Data Leaves Unanswered
Qualified cells can be incorporated into a poorly designed pack. Connections, insulation, protection thresholds and enclosure temperatures need their own assessment. Cell-level performance data can support pack development, but cannot alone demonstrate final usable energy, connector heating or fault response.
Do not demand an IP67 rating, liquid-cooling test or propagation test for every pack without an application basis. Instead, establish which requirements apply and identify where each is verified. The appropriate evidence for a small portable instrument differs from that for a vehicle or stationary installation.
2.2 What Pack-Only Data Leaves Unanswered
Confirm which cells the pack report evaluated and whether the supplied pack uses an approved cell option. A report for one cell model cannot be silently applied to another because both have the same nominal voltage or capacity.
Cell incoming inspection and supplier controls support production consistency. Buyers may request agreed checks for identity, appearance, dimensions, voltage, resistance and capacity sampling. Do not prescribe a particular vision system, defect resolution or inspection speed unless it is part of the agreed process.
A design report normally covers specified qualification samples, not an entire production lot. Link the approved design to production records through configuration control and traceability rather than expecting one certificate to identify every shipped cell.
Part 3: Verifying Cell Test Reports
3.1 Check Identity, Conditions and Acceptance Criteria
Verify manufacturer, exact model, ratings, sample identification and test dates. Read the specification used for acceptance, including rated versus minimum capacity. Confirm charging method, rest time, discharge current, temperature and cutoff voltage before comparing results.
There is no universal rule that a capacity retest must be within 5% of nominal or use a 0.2C discharge. Use the approved specification and test method. A result below a guaranteed minimum requires investigation under the agreed acceptance process.
For cycle-life data, confirm charge and discharge rates, depth of discharge, temperature, rest periods and the endpoint criterion. Distinguish measured results from projections and cell-level data from pack runtime claims. Avoid converting a chemistry name into a fixed cycle-life promise.
3.2 Review Safety Tests Without Confusing Sampling and Screening
Check the applicable standard, edition, clauses, sample allocation, conditioning and acceptance criteria. Note exclusions, deviations, interrupted tests and supplemental reports. A “PASS” is meaningful only within that defined scope.
Do not require every saleable cell to undergo destructive abuse testing. Such tests normally use designated samples. Production screening instead uses defined, generally non-destructive checks and sampling plans. Neither routine voltage inspection nor a destructive test on one sample establishes that every unit is defect-free.
Request supporting measurements where appropriate to the purchasing decision. Share confidential technical reports through an agreed access process. If authenticity is uncertain, contact the issuing laboratory through independently verified details and obtain authorization where needed.
Part 4: Verifying Pack Test Reports
4.1 Match the Report to the Finished Assembly
Compare the reported pack model and drawings with the purchase specification and bill of materials. Review series/parallel configuration, approved cells, enclosure, insulation, connector, fuse and protection hardware. Identify relevant firmware and parameter revisions where software affects protective behavior.
Verify the reported electrical and environmental ratings against intended use. Temperature cycling, vibration, shock, ingress and insulation requirements depend on the application and standard. Do not copy a universal temperature range, insulation-resistance limit, IP rating or “120% SOC” cutoff into every purchasing specification.
For protection evidence, distinguish normal charger regulation from fault cutoff. A BMS or PCM test should identify the evaluated function, threshold, tolerance, response and recovery conditions. Approved signal simulation can support functional testing; hazardous cell overstress is not an ordinary receiving-inspection procedure.
4.2 Separate Qualification from End-of-Line Records
Qualification evaluates the design. End-of-line testing checks production units against approved release criteria. Suitable checks may include identity, polarity, voltage, function and communication; insulation or leak testing applies where specified by the design.
Do not assume every pack has contactors, a coolant circuit or a vehicle identification number. A pack serial number, lot code or other controlled identifier may provide appropriate traceability. Define how it links to the assembly revision, cell lots and inspection results.
Where the supplier claims 100% inspection, reconcile shipped unit identifiers with completed records. Review missing entries, failures, rework and retest disposition. Do not require peak-current burn-in or discharge to one fixed shipping state of charge for every application; validate production tests and determine shipping conditions separately.
Part 5: Standards, Authenticity and Change Control
5.1 Check the Right Scheme and Product Scope
Portable, industrial and automotive batteries have different standards and product scopes. Confirm requirements with the responsible compliance team for the intended market. An automotive cell report is not automatically the appropriate requirement for a medical instrument or an industrial sensor.
For UL claims, verify the file, exact model, category and certification status through the issuing scheme. UL’s component-recognition guidance explains that component recognition supports end-product evaluation and includes conditions of acceptability. A recognized cell does not automatically make the assembled pack or host device UL certified. Testing to a UL standard by another body is not the same as certification issued by UL.
For laboratory-accredited results, check the specific test activity and site against the accreditation scope. ILAC’s guidance on accredited bodies explains scope verification and contacting the relevant accreditation body. Do not infer that every report from an accredited organization was issued within its accredited scope.
For transport, request the applicable UN 38.3 evidence for the cell or battery design. Applicability, test sequence and provisions vary with the item. Do not treat all eight tests as mandatory for every cell and pack, or assume cell evidence alone always covers an assembly. PHMSA’s lithium-battery guidance provides an official starting point for U.S. transport requirements. Packaging and shipment documentation remain separate obligations.
5.2 Review Changes Rather Than Assuming Automatic Expiry
A report records the samples tested at a particular time. It does not universally expire after a fixed number of years. Certification status, scheme rules, standard transitions, customer requirements and design changes can affect its current acceptability.
Changes to cells, protection settings, firmware, wiring or enclosure require an impact assessment. Some variants may already be covered; others may need additional evaluation, an amendment or retesting. Obtain a documented determination from the responsible certification body or laboratory when applicable. Neither “all changes invalidate everything” nor “same voltage means no retest” is a reliable rule.
Red flag | Buyer response |
|---|---|
Only a certificate cover page | Request model scope, supporting report references and limitations |
Different cell or pack model | Request approved variant coverage or a change assessment |
Unsupported laboratory logo | Verify issuer, report identity and relevant accreditation scope |
Missing production linkage | Request agreed lot or unit mapping and release records |
Unexplained standard or edition | Confirm applicability to the application and target market |
Use a release checklist that names required documents, revision identifiers, unresolved gaps and approval owners. Absence of ISO 9001 certification does not by itself prove there is no traceability; verify the actual process and records.
When discussing a custom battery project with Large Power, define the application, market and required evidence at the quotation stage. Review testing and certification capabilities against the particular activities needed; do not assume a general capability statement establishes approval for an individual model.
The purchasing decision should rest on a documented chain from qualified cells to the approved pack and the delivered goods. Close gaps before shipment, and retain the evidence needed to assess future substitutions or field issues.
FAQ
Does a cell report cover the battery pack?
Not automatically. It may support the pack assessment, but the assembled configuration, protection and intended use require their own evidence. Confirm what the applicable scheme permits.
Is a test report the same as a certification certificate?
No. A report records defined testing, while certification is issued under a scheme with a specified scope. A transport test summary and a production inspection record have different purposes again.
Should every cell undergo abuse testing before shipment?
No. Destructive tests normally use designated qualification samples. Production screening follows an approved inspection plan and should not damage saleable units.
What capacity difference should trigger rejection?
Use the agreed minimum specification and test conditions, including uncertainty where relevant. There is no universal 5% tolerance for all cells or packs. Investigate results against the purchase acceptance criteria.
Does any customization invalidate the report?
No. Assess the specific change and existing coverage. Depending on the design and scheme, an approved variant, report amendment or additional testing may be appropriate.
How can OEM buyers verify laboratory accreditation?
Use the accreditation body’s directory to check status, laboratory site and the specific test scope. Accreditation is not blanket product approval, and it does not mean every activity offered by the laboratory is accredited.


