

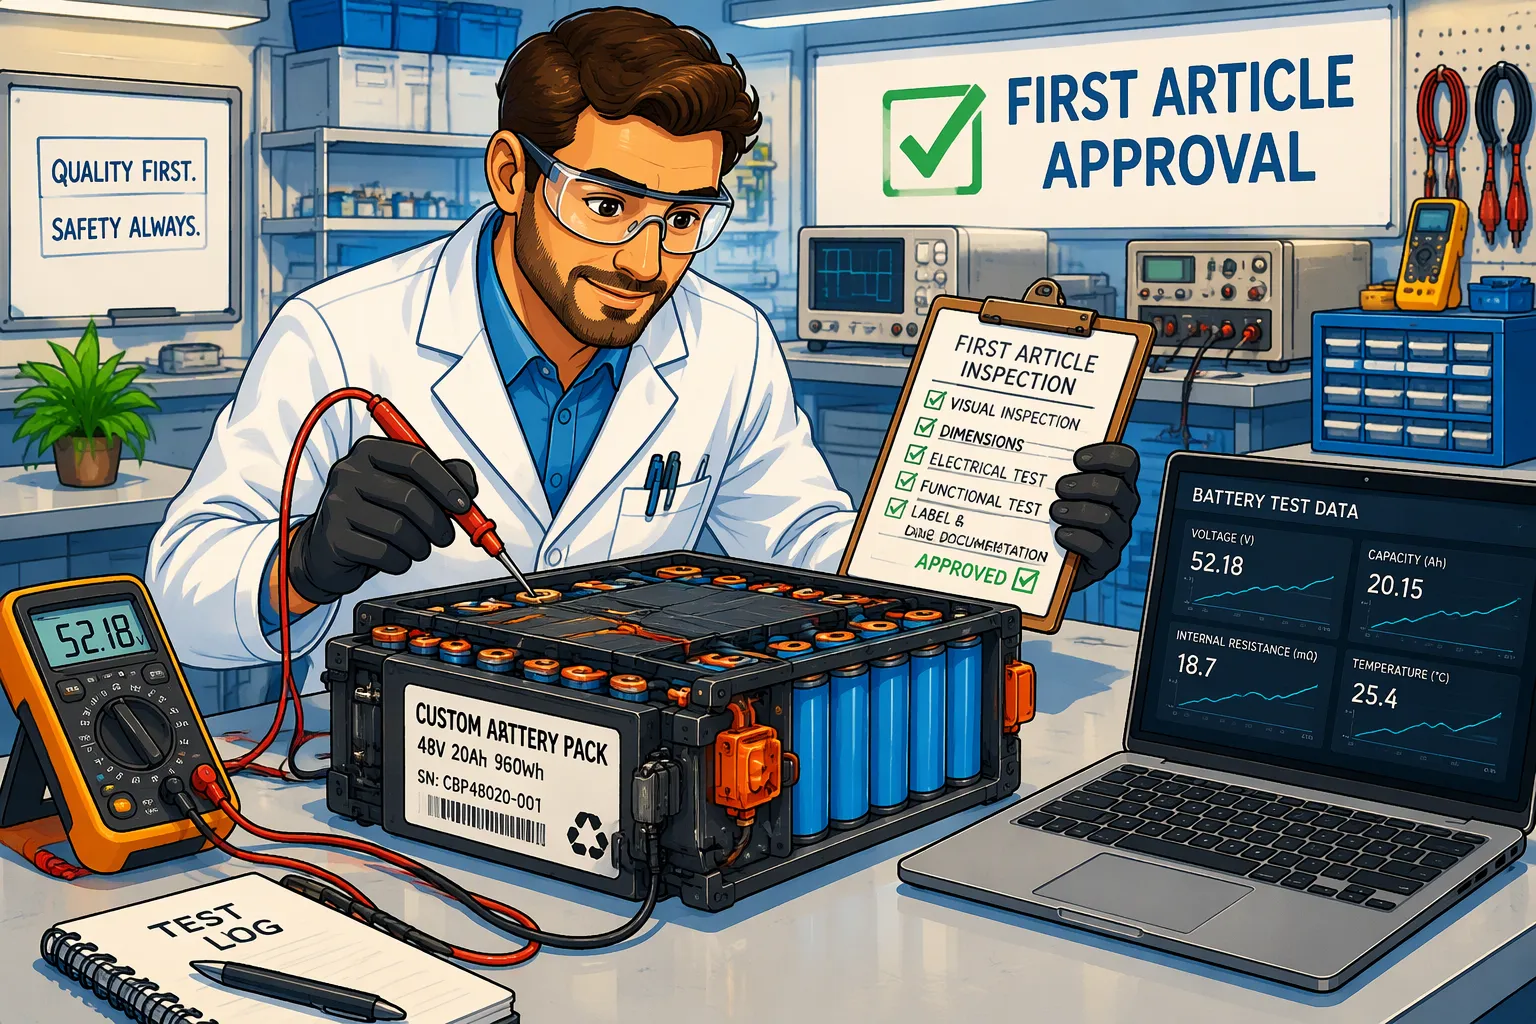
Quick Answer: Before approving a first-article battery pack, verify it against the released drawings and specification, including fit, pinout, firmware, labels and test records. Document deviations and the evidence needed to close them before authorizing production.
Approval matters. Your signature locks in tooling, firmware, and BMS configuration. A missed check turns into a mass-production defect.
This post gives you specific criteria for each check, plus a documentation and change-control process for Custom Battery Pack Sample Approval.
A first article is a tooling-validated reference unit built to released drawings and BOM. Pilot production validates process capability.
Key Takeaways
Make sure the sample matches the drawings and BOM exactly. Check the mounting points, connectors, and labels.
Test the pack while it powers a real device. Watch for voltage sag and make sure the BMS protection works.
Check how much the temperature goes up at peak load. Also check how long the battery lasts under a real duty cycle. Heat can make the battery fail early.
Check that the charger works with the pack, and test the pack inside your device. Even small voltage errors can make the pack last a shorter time.
Gather all test reports, including UN 38.3, and keep a golden sample. Control changes to prevent defects.
Part1: Mechanical Fit and BOM Conformance
1.1 Enclosure Fit and Connector Mating
Begin with the drawing package and the BOM. Make sure the first article matches both, line by line. Check every mounting point, screw boss, and bracket against the released drawing. Then look at the installed envelope: connector body height, cable bend radius, latch clearance, and room for insertion and removal. A connector can be right on paper and still fail because the latch hits a chassis member or the cable exits into a sharp bend, as goldencellpower.com notes for robot packs.
Connector mating needs its own review. Confirm the host-side mating half, current rating, keying, locking method, cable exit direction, and service disconnect procedure. Zerne Battery recommends checking polarity, pinout, strain relief, and mechanical retention before approval. Ask whether vibration can loosen the connection and whether the latch stays secure after repeated mating cycles.
Fit expectations differ by market. A medical device housing leaves little room for tolerance stack-up. A robotics chassis mount must survive vibration. Security camera enclosures and consumer electronics shells are tight and cosmetic. Infrastructure brackets and industrial equipment bays favor service access. Representative robot packs from goldencellpower.com range from 228×105×75 mm to 640×620×110 mm, so never assume one envelope fits another.
1.2 Cell Records and Labeling
Record cell-level data during sample approval. Log open-circuit voltage (OCV), appearance, size, and weight for each cell. These records give you a baseline for incoming inspection later. They also show cell supply changes before they reach mass production.
Check labeling against the drawing package. Verify chemistry, capacity, voltage, polarity marks, and warning text. Confirm the label survives the intended environment. A missing or wrong mark becomes a safety and traceability problem in the field.
Part2: Electrical Performance Under Load
2.1 Load Profile and Voltage Sag
A basic discharge test does not show you much about how the pack acts in real use. Instead, test the first article using the actual load profile of the device. Put meters on the real device and record the steady current, short peaks, duty cycle, and the voltage range the device can handle during charge and discharge, as tefoobattery.com suggests. This profile shows the real peak-to-average ratio, which sets your C-rate requirement. It also shows the lowest voltage before the device shuts down, which sets your series count.
Follow a clear measurement sequence:
Measure the battery current at the terminals while the device runs in a typical way.
Record standby current, average current, worst-case steady current, peak level, pulse length, pulse rate, startup, stall or jam current, regen current, and shutdown voltage.
Repeat the measurement at low battery voltage and at the highest expected room temperature, because converter and motor current can go up as pack voltage drops.
Use the final device and typical firmware, then record voltage sag and shutdown behavior.
Cover every operating mode: normal use, maximum load, startup and shutdown, standby and sleep cycles, charging while installed, repeated use, and realistic temperatures, per zerne-battery.com. Pay close attention to voltage sag. Too much sag can cause device resets, weak motor performance, or early low-voltage protection even when nominal capacity looks fine. Before you test, write pass/fail limits for runtime, sag, peak current, BMS recovery, temperature rise, charger behavior, and production repeatability.
Chemistry sets the context for these limits. Cell-level reference ranges include LiFePO4 at about 3.2 V nominal and 90–120 Wh/kg, and conventional Li-ion (NMC, LCO, LMO) at about 3.6 V nominal and 150–180 Wh/kg. Treat these as cell-level context only, never as pack guarantees.
2.2 BMS Protection and Firmware
The BMS limits must match the exact cell specification. Generic voltage and temperature thresholds can shorten life or create safety risk, calb-battery.us notes. Check each protection function against the approved specification:
Protection Function | Why It Matters |
|---|---|
Overcharge protection | Helps control risk under abnormal high-voltage conditions |
Over-discharge protection | Prevents cells from being excessively discharged |
Discharge overcurrent protection | Controls overload and fault conditions |
Charge overcurrent protection | Helps manage abnormal charging current |
Short-circuit protection | Responds to serious fault conditions |
Temperature protection | Limits charging or discharging under unsafe temperature conditions |
Cell balancing | Helps manage voltage differences in series-connected cells |
Recovery logic | Defines how the pack restarts after protection occurs |
Confirm the exact thresholds, delays, and recovery conditions in the engineering specification, then check them by testing.
Communication needs proof, not just a datasheet claim. A CAN interface listed on a BMS datasheet is never proof of controller compatibility, dlcpo.com warns. Ask for the actual protocol documents and validation records for your controller model. Ask for a communication matrix covering firmware version, baud rate, register map, and tested controller list.
Finally, lock the BMS configuration record: hardware version, firmware version, parameter version, protocol version, protection settings, calibration data, update method, access control, and change approval process. Any change to protection parameters, firmware, communication, MOSFETs, or sensing design may need revalidation and your approval.
Part3: Thermal and Runtime Validation
3.1 Temperature Rise at Peak Load
Heat is the slowest problem to appear and the easiest to miss in a short bench test. Measure the temperature rise at the cell, the BMS, and the enclosure surface under both continuous and peak load. Compare each reading against your thermal design limits. Epec Tec notes that a good load profile defines continuous current, peak current, pulse duration, duty cycle, operating temperature, and voltage limits. Test the finished pack under those real conditions to catch overheating and faster aging early.
Sensor accuracy matters when you are judging a small margin. A Nature study on lithium-ion thermal modeling reports NTC thermistors with a systematic accuracy of ±0.2 °C and a combined measurement uncertainty of roughly ±0.27 K per sensor. That study checked its model against a 3 C discharge at 9 A. Treat readings inside that uncertainty band as unclear, not as a pass. For a medical device or a security camera running all the time, a small but steady rise at the BMS can shorten service life. For a robotics chassis or an industrial equipment bay, peak pulses cause the worst-case heat.
3.2 Runtime Against Duty Cycle
A single continuous discharge tells you little about runtime in the field. Run the test against the real duty cycle and record the conditions: ambient temperature, load profile, and cutoff voltage. VTC Batt lists the inputs you need before testing:
Design Item | What to Provide |
|---|---|
Required runtime | Hours, days, or operating cycles |
Average current | Typical operating current |
Standby current | Current during sleep or idle mode |
Duty cycle | Percentage of time active versus standby |
Operating temperature | Expected operating range |
Device cut-off voltage | Minimum operating voltage |
VTC Batt gives the estimate as average current = active current × duty cycle + standby current × (1 − duty cycle), and runtime ≈ usable capacity ÷ average current. Treat this as a starting estimate only. VTC Batt also warns that runtime depends on average current, while stable operation depends on peak-load capability. Check peak current, pulse duration, and inrush current separately. Temperature limits also change results: VTC Batt cites a typical LiPo range of 0°C to +45°C charging and -20°C to +60°C discharging, with actual limits set by the chosen cell.
Chemistry changes the expected thermal profile. LiFePO4 favors thermal stability and cycle life, NMC favors energy density, LCO suits compact high-energy designs, and LMO suits high-power pulses. Cell-level references include LiFePO4 at about 3.2 V nominal and 90–120 Wh/kg, and conventional Li-ion (NMC, LCO, LMO) at about 3.6 V nominal and 150–180 Wh/kg. Use these as context, never as pack guarantees.
Part4: Charger and Controller Compatibility
4.1 Charge Profile and Cutoff
The charger has to match the cell datasheet, not just a general chemistry label. Totex Manufacturing reports that a charge voltage error of only 50 to 100 mV can cut a lithium-ion pack’s cycle life by 20 to 40 percent. That margin is well inside the tolerance of many off-the-shelf chargers, so check the actual output instead of the nameplate.
Parameter | Requirement |
|---|---|
Constant current until the termination voltage, then constant voltage with current taper to a cutoff of typically C/20 or C/10 | |
Termination accuracy | Ideally within plus or minus 0.5 percent of the target voltage |
Li-ion and LiPo charge voltage | 4.20 V per cell plus or minus 50 mV, at a maximum rate of 0.5C to 1C |
LiFePO4 charge voltage | 3.60 V per cell with proper CC/CV |
High-voltage Li-ion (4.35 V and above) | Needs regulation of plus or minus 1 percent or better; not compatible with standard 4.20 V chargers |
Also confirm the communication handshake. Make sure the SMBus, I2C, or CAN protocol, register map, and baud rate match the approved firmware version. A pack that charges correctly but reports the wrong state of charge will still fail in the field.
4.2 In-Equipment Integration Testing
Bench tests do not prove compatibility. Require testing inside your own equipment, and link every result to the test conditions. Cover installation, startup loads, runtime, charging, and controller behavior in one continuous sequence.
Watch for problems that only show up in the host. A medical device may pull a brief inrush current at power-on that trips the BMS. A robotics controller may read pack data over CAN during motor acceleration and act up when voltage sags. A security camera on permanent charge may never finish a full cycle, so check the float behavior against the cell datasheet.
Record the ambient temperature, load profile, cutoff voltage, and firmware version for each run. Ask the supplier to sign the same test record. Any mismatch between charger behavior and approved firmware becomes a change-control item before you approve the sample.
Part5: Factory Test Data and Receiving Checklist
5.1 Test Report and UN 38.3 Review
Look over the first-article test report and compare it to the approved test requirements before you sign anything. The report should show the tests you asked for, the conditions used, and the results. A capacity or discharge report shows how the pack did on factory test equipment. It cannot tell you if the pack works with your wiring, controller software, and charging setup, so treat it as one input, not the whole case.
Make sure the UN 38.3 test documentation is on file. Epec Tec describes the package you should get: a 10-page test report and a test summary. The report has the applicant’s name and address, the battery manufacturer’s name and address, the number of samples received and the date, and the testing completion date. It also lists technical details such as voltage and rated capacity, plus the test parameters, equipment, methods, and results.
The summary has its own rules. Intertek notes that a test summary must be available from the shipper upon request, and it must carry the name and title of the signatory as an indication of validity. Collect test reports from your cell vendors and subcontractors so the summary covers the whole pack, not just the assembled unit.
5.2 Receiving Checklist and Deviations
Build a receiving checklist that covers drawings, fit, wiring, firmware, test records, and deviations. HNF Battery lists the product identity items to confirm on arrival: exact model, chemistry, cell count or configuration, voltage, capacity, watt-hours or lithium content, pack mass, and condition. Add the shipment description, the UN 38.3 summary, the current safety data sheet, and the transport classification.
Log every deviation with a disposition. Record the sample ID, BMS firmware version, and equipment software version, so you know both tests used the same configuration. Note the load sequence, starting state of charge, temperature, and any alarms. Ask the supplier to return the checklist marked provided, not applicable, or pending, with a file reference and a responsible party.
Supplier capability deserves the same scrutiny. Totex Manufacturing holds ISO 9001, ISO 13485, and ISO 14001 certification, and the ISO 13485 standard page describes a system built around documentation, risk management, and corrective action. Medical OEMs commonly require it when qualifying suppliers.
Certification | What It Covers |
|---|---|
ISO 9001 | General quality management system |
ISO 13485 | Quality system for medical devices; certifies the system, not the product |
ISO 14001 | Environmental management |
Confirm one manufacturer can design, test, and build the pack, and confirm cell supply consistency. Settle tooling scope, NRE deliverables, design inputs, and test requirements before you approve tooling and NRE costs. A connector that fits does not mean the two match: the 40135 8S1P 20Ah pack has a maximum charge voltage of 29.2 V and a maximum charge current of 15 A, so the charger must stay within both limits. This discipline is the heart of Custom Battery Pack Sample Approval, and it protects every later lot.
Part6: Custom Battery Pack Sample Approval and Change Control
6.1 Approval Record and Golden Sample
Write down the Custom Battery Pack Sample Approval using photos, measurements, and test notes. Keeppower suggests logging open-circuit voltage, appearance, size, and weight for each cell. Also record an initial capacity check, charge behavior, and discharge under the expected load. For the pack itself, confirm BMS behavior, balance lead access, connector model, cable length, polarity, insulation, labeling, and packaging.
Insulation should get its own line in the record. Check the sleeving itself, not just the wire. Confirm the wall thickness, shrink ratio, and temperature rating of the heat shrink tubing over nickel tabs and balance leads. Make sure it stays intact after a full charge-discharge cycle at the pack’s rated current.
Keep a golden sample as the reference standard. Store it with the signed checklist, the deviation log, and the drawing package. A medical device OEM, a robotics builder, or a security camera maker can then compare every later lot against one known unit.
6.2 Change Control to Mass Production
Set change-control trigger points before you release the pack. Any cell, BMS, firmware, connector, or drawing change needs re-approval. Treat the baseline as a traceable set of approved revisions, not a single undated sample.
Change Control Trigger Point | Required Action |
|---|---|
A cell change | Run an impact assessment and update affected records |
Changes affecting functions, risk controls, or approval scope | Document regression testing, validation, or scheme review |
Remaining changes and deviations | Manage through an authorized process |
Keep first-article approval separate from pilot production approval. The first article is a tooling-validated reference unit built to released drawings and BOM. Pilot production validates process capability. Move from one to the next only when the pilot line holds the approved dimensions, firmware version, and test limits across a full run, and when every deviation carries a closed disposition.
Think of Custom Battery Pack Sample Approval as a step you repeat every time. First, check that the BOM and drawings match and that the pack fits. Then run load tests, thermal and runtime checks, and charger and controller compatibility tests. Review the test data, including UN 38.3 documents, and sign off in writing.
This step sets your reference; it is not just a formality. The approved sample, its records, and the golden sample become the baseline for every production lot.
Next, give a conditional or full approval. Set pilot production criteria and change-control trigger points. Store the golden sample, signed checklist, and deviation log with the drawing package.
FAQ
What separates a first article from pilot production?
A first article is a reference unit that has been checked by tooling and built to released drawings and BOM. Pilot production proves your process can repeat that unit across a full run. Approve the first article first, then move to pilot production only when dimensions, firmware, and test limits hold across the run.
How long should load testing take?
Test until the pack completes your real duty cycle at the expected ambient temperature, not for a fixed clock time. Record voltage sag at continuous and peak current, plus BMS recovery after each protection event. Stop only when every pass/fail limit in your test plan has a recorded result.
Which documents should I collect before signing?
Collect the first-article test report, the UN 38.3 test report and test summary, the BMS configuration record, and the signed receiving checklist. Add the deviation log with a disposition for each item. File everything with the drawing package and the golden sample.
When does a change require re-approval?
Any change to the cell, BMS, firmware, connector, or drawing triggers re-approval. Treat protection thresholds, communication protocol, and MOSFET selection as part of that list. Run an impact assessment, then repeat the affected tests before you release the lot.
Can I approve a sample with open deviations?
Yes, with conditions. Issue a conditional approval that names each open deviation, its disposition, and the owner. Full approval follows only when every deviation closes and the pilot line holds the approved configuration. Never let an open deviation pass silently into mass production.
For a new OEM design, share the released drawings, acceptance criteria, and unresolved deviations when you discuss custom battery pack prototyping and validation with the supplier.


